Start of production in Ingolstadt
Audi integrates A2 e-tron into existing production

For the new electric model, the manufacturer is relying on existing facilities, joint body production with the A3 and fewer parts variants. More than 1,200 production components are being reused or further used.
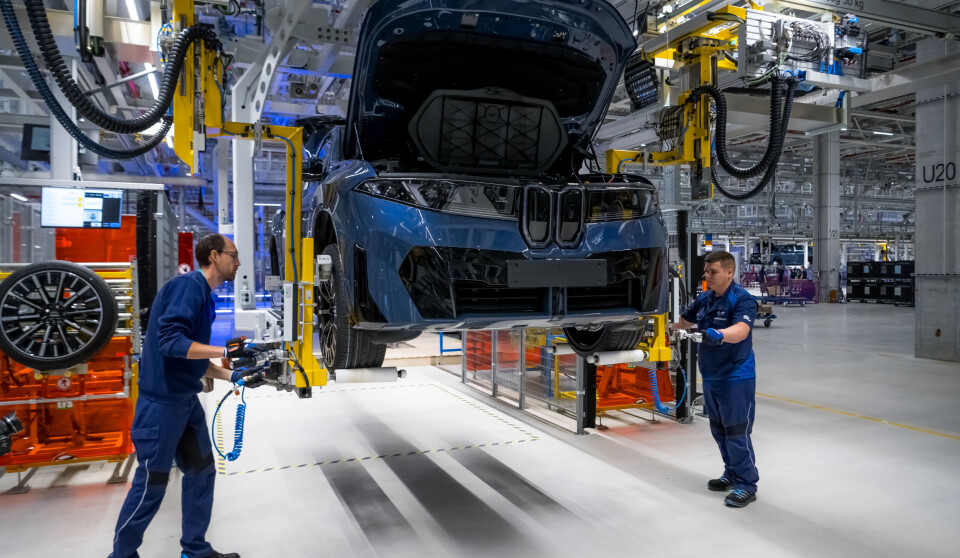
Rather than setting up an entirely new production line, Audi has focused on integrating the A2 e-tron as efficiently as possible into existing manufacturing structures at its Ingolstadt plant. A significant share of the production equipment is being reused. More than 1,200 components, including robot welding guns and around 250 robots previously used for other Audi models, have been repurposed for the new EV.
Ingolstadt currently operates three assembly lines, with the A2 e-tron launching on assembly line 2. The line previously built the Audi A4 before production of its successor, the A5, was transferred to Neckarsulm. That move freed up capacity and floor space in Ingolstadt, allowing Audi to prepare the line for the A2 e-tron largely without interfering with production on the plant’s other two assembly lines.
The approach reflects a growing challenge for established automotive plants: bringing new vehicles and powertrains into existing factories without building dedicated production facilities for every new model.
Audi used weekends and plant shutdown periods for the necessary conversion work in order to avoid disrupting ongoing series production. In the body shop, much of the reused equipment comes from A3 production and in some cases only had to be relocated rather than replaced. The same principle applies in the paint shop, where the A2 e-tron is processed alongside the electric A6 e-tron and Q6 e-tron.
A2 e-tron and A3 share body production

This is particularly evident in the body shop, where Audi builds A2 e-tron bodies alongside those of the A3. The flexible layout of the existing production equipment enables the two models to share manufacturing capacity. This kind of flexible mixed production on existing lines is becoming increasingly important as OEMs adapt plants to different powertrains and changing volumes.
The two models do not share the complete body production process from the outset. Their platforms are initially built on separate lines before converging on a common framing and body assembly line, where the bodies are completed. Audi uses a combination of shared tooling and flexible production equipment, allowing the line to switch between A2 e-tron and A3 bodies from one production cycle to the next.
Audi has not disclosed the overall share of newly installed equipment in the A2 e-tron production setup. However, the extensive reuse of existing production assets remains a key part of the manufacturing concept.
At the same time, Audi is increasing automation levels. The A2 e-tron introduces fully automated wheel assembly to Ingolstadt for the first time. Robot stations in front- and rear-axle pre-assembly replace the semi-automated bolting stations previously used in this area.
The wheels are automatically transported to the installation point and supplied with the required bolts before robots position them precisely on the vehicle. Two integrated cameras determine the exact position of the brake disc or brake drum. The system then carries out the fastening process using defined parameters, with the tightening data recorded for full traceability. Audi says the setup is intended to improve process reliability and quality while also reducing ergonomic strain for operators.

Further automation has also been introduced in the body shop. Audi is using bin-picking technology, with camera-guided robots identifying and picking components directly from unsorted containers. According to the carmaker, the system can now also handle small sheet-metal parts and feed them directly into the production process. This also reduces the need for ergonomically demanding manual handling.
Lower complexity simplifies logistics
A second focus is reducing product and process complexity. Audi says the A2 e-tron requires fewer production-related part numbers than previous vehicle projects.
According to Audi, the number of part numbers relevant to production and logistics has been cut by 50%. The reduction simplifies material supply and logistics processes and also allows the carmaker to reduce the space required for material supermarkets, storage and sequencing.
Audi is also introducing the so-called pearl-chain production principle in Ingolstadt for the first time, following its use at the Neckarsulm plant. Under this system, the sequence of customer orders is fixed six days before assembly begins and then maintained throughout the production process.
Previously, the final sequence of the relevant vehicle orders was only determined a few hours before assembly. Fixing the sequence six days in advance gives Audi considerably more planning certainty and allows logistics processes to be aligned with actual demand much earlier. The carmaker says this can reduce logistics space requirements by up to 25%, mainly through less sequencing and more demand-oriented material control.
This allows suppliers to manufacture and pack components in the exact sequence required on the assembly line. As a result, Audi can reduce the need for additional storage and sequencing areas inside the plant. The system reflects the growing importance of smart sequencing in modern vehicle assembly, particularly as model and variant complexity increases.
Edge Cloud replaces more than 450 industrial PCs
The IT architecture supporting production is changing as well. For the A2 e-tron, Audi is using its Edge Cloud 4 Production to provide production applications centrally.
The universal testing system used to commission vehicle control units, as well as digital operator guidance for vehicle-specific assembly tasks, are both managed through the cloud. According to Audi, this eliminates the need for more than 450 industrial PCs in assembly.
Instead of running individual shopfloor applications locally on industrial PCs, the computing is now handled by virtual machines in Audi’s cloud infrastructure. Audi says the virtualised setup can reduce both investment and process costs while also lowering energy consumption.
Moving these applications away from individual shopfloor computers towards a central infrastructure is intended to simplify software updates, maintenance and the rollout of new functions. For Audi, the A2 e-tron is therefore also another step towards a more software-driven and connected production system.
The approach is not limited to assembly. Audi is also virtualising control systems in the body shop. Edge Cloud 4 Production is already running in high-volume body production for the Audi A5 and A6 at the Neckarsulm plant, providing a further application case for the technology beyond the A2 e-tron.
The company is complementing this with AI-based knowledge tools. A supply chain chatbot gives employees access to information on processes and documentation, while the so-called mAIntenance Chat supports maintenance teams with fault analysis and troubleshooting.
Development time cut by 21 months
Audi has also shortened the product development process for the A2 e-tron. From the start of development to series production readiness, the programme took 21 months less than previous vehicle projects.
The carmaker attributes the shorter timeframe to experience gained from earlier launches, streamlined coordination processes and a higher level of vehicle maturity at an earlier stage of pre-series production.
For Gerd Walker, Audi board member for production and logistics, the project goes beyond the launch of a single model. “With the A2 e-tron, we are also showing that it is possible to build cars economically in Germany,” he said. Flexible production systems, AI applications and workforce expertise are central elements of the approach.
For Ingolstadt, the A2 e-tron is therefore also a test of how effectively a new EV can be integrated into an established plant using existing equipment, lower complexity and a leaner logistics setup. The additional details from the ramp-up show that Audi is relying less on major new infrastructure than on freed-up capacity, equipment reuse, flexible tooling and tighter production and logistics control.